Custom Parameters 1
Select Technology Parameters and choose Laser Technology to view/edit Custom parameters 1.
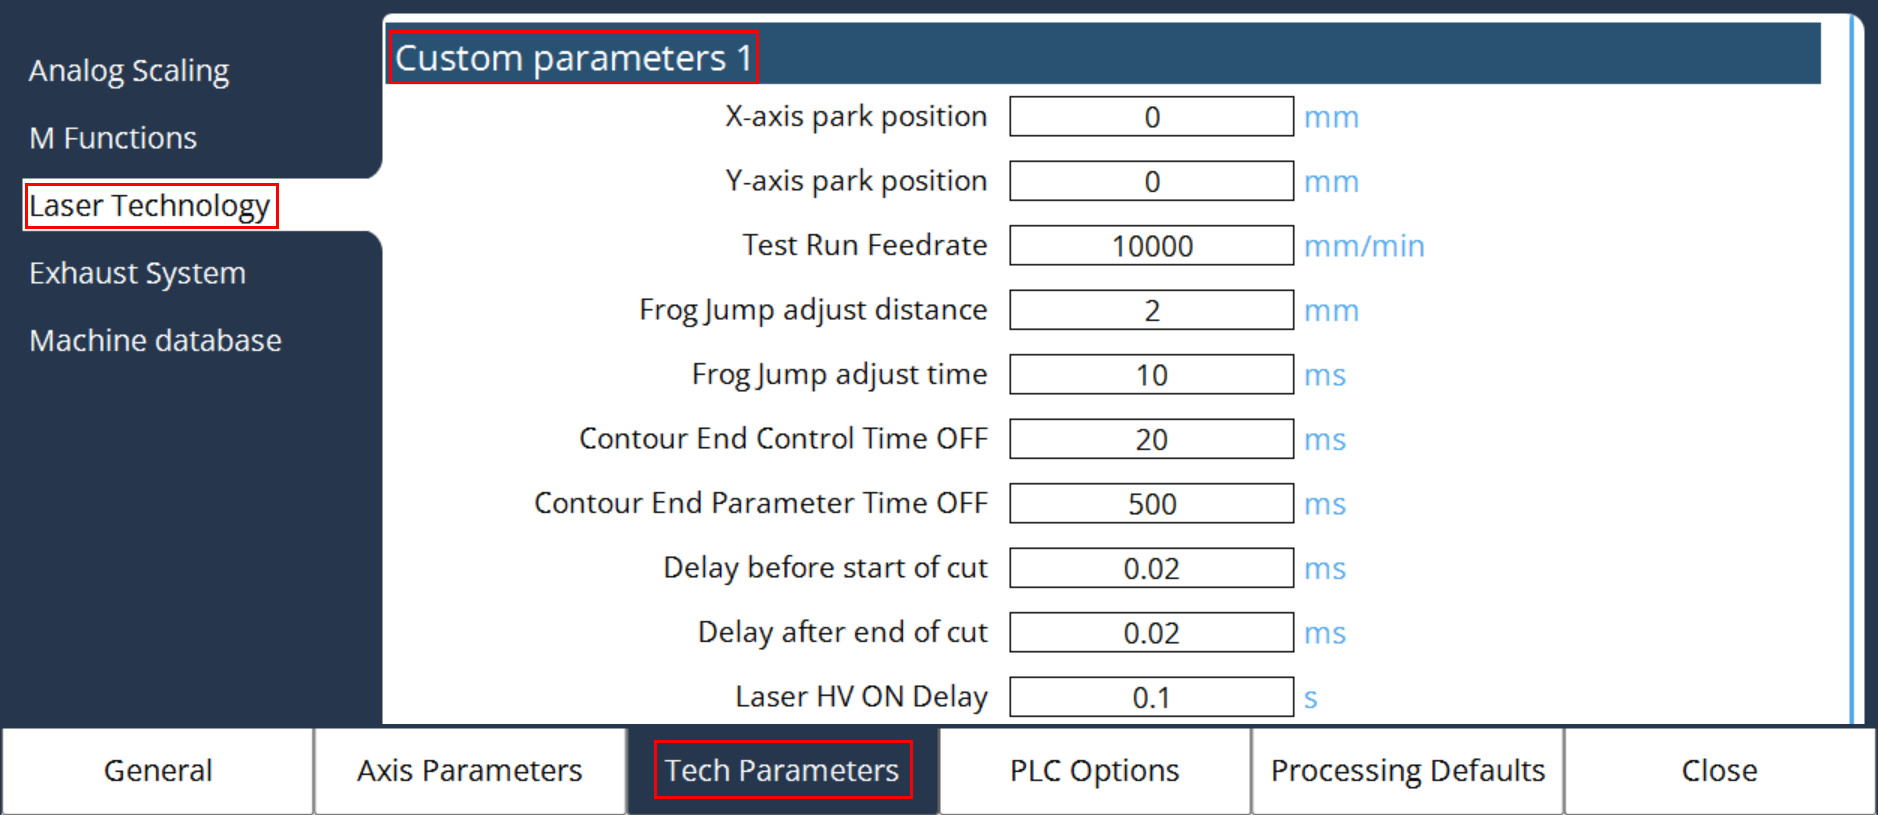
Custom parameters 1 contains 10 entries which are stored one to one in the parameter field from P760-P769 and can be used there arbitrarily.
X-axis park position (P760)
This is the X-axis Park position value in mm, used in the Park Position program.
Y-axis park position (P761)
This is the Y-axis Park position value in mm, used in the Park Position program.
Test Run Feedrate (P762)
It is the speed assigned for Test Run in mm/min. Test run works only with X and Y axis movements and Z axis will be locked. Laser power and assist gas is not required for Test run.
Frog Jump adjust distance (P763)
It is the adjust distance in mm between contours in a program, to start positioning the cutting head to next point. For ex: P763 = 4mm, and the distance between the contour is 10mm, then when the cutting is finished in the current contour, the head moves up and start position for the next contour 4mm before the destination point. Suppose if the distance between the contour is < 4mm, then the positioning will happen based on the time.
Frog Jump adjust time (P764)
It is the adjust time in ms between contours in a program, to start positioning the cutting head to next point. For ex: P764 = 20ms, and the time taken between the contour is 100ms, then when the cutting is finished in the current contour, the head moves up and start position for the next contour 20ms before the destination point.
| The Frog Jump is adjusted in 2 modes as distance & time, whichever comes first will activate the head motion. Hence based on the Machine dynamics, an appropriate value should be assigned. |
Contour End Control Time OFF (P765)
It is the adjust time in ms before the end of contour completion (M15 command), to control the contour end functions such as height control freeze, beam off etc., For ex: P765 = 20ms, if the end functions are activated, then it will be enabled 20ms before the end of contour.
| Primarily, this function will be activated based on the distance specified in the Laser DB, if the distance is lesser than the contour length, then it will be activated based on this time. |
Contour End Parameter Time OFF (P766)
It is the adjust time in ms before the end of contour completion (M15 command), to activate the 'End Parameters'.
For example: P766 = 100ms, if the End Parameter function is activated then the last 100ms contour length will be processed with 'End Parameters'
| Primarily, this function will be activated based on the distance specified in the Laser DB, if the distance is lesser than the contour length, then it will be activated based on this time. |
Delay before start of cut (P767)
This is the wait time in ms followed by M14 command to start the contour motion.
Delay after end of cut (P768)
This is the wait time in ms followed by M15 command to go to next contour position.
Laser HV ON Delay (P769)
This is the delay time in secs, between the Laser Controls ON and Power Supply ON output. It is required for some type of oscillator such as IPG.