Configuration of Laser Power Control (LPC)
An Analog axis control module in the controller is configured as Spindle axis, to control the laser power analogue output depends on the path velocity. Since the properties of Spindle axis are defined to handle this special function, here it is called as LPC. It is possible to have 2 LPC as LPC1 & LPC2. With Add Axis, when LPC1 is selected, the axis properties are assigned automatically and only need to select the Axis Connection & Axis Address.
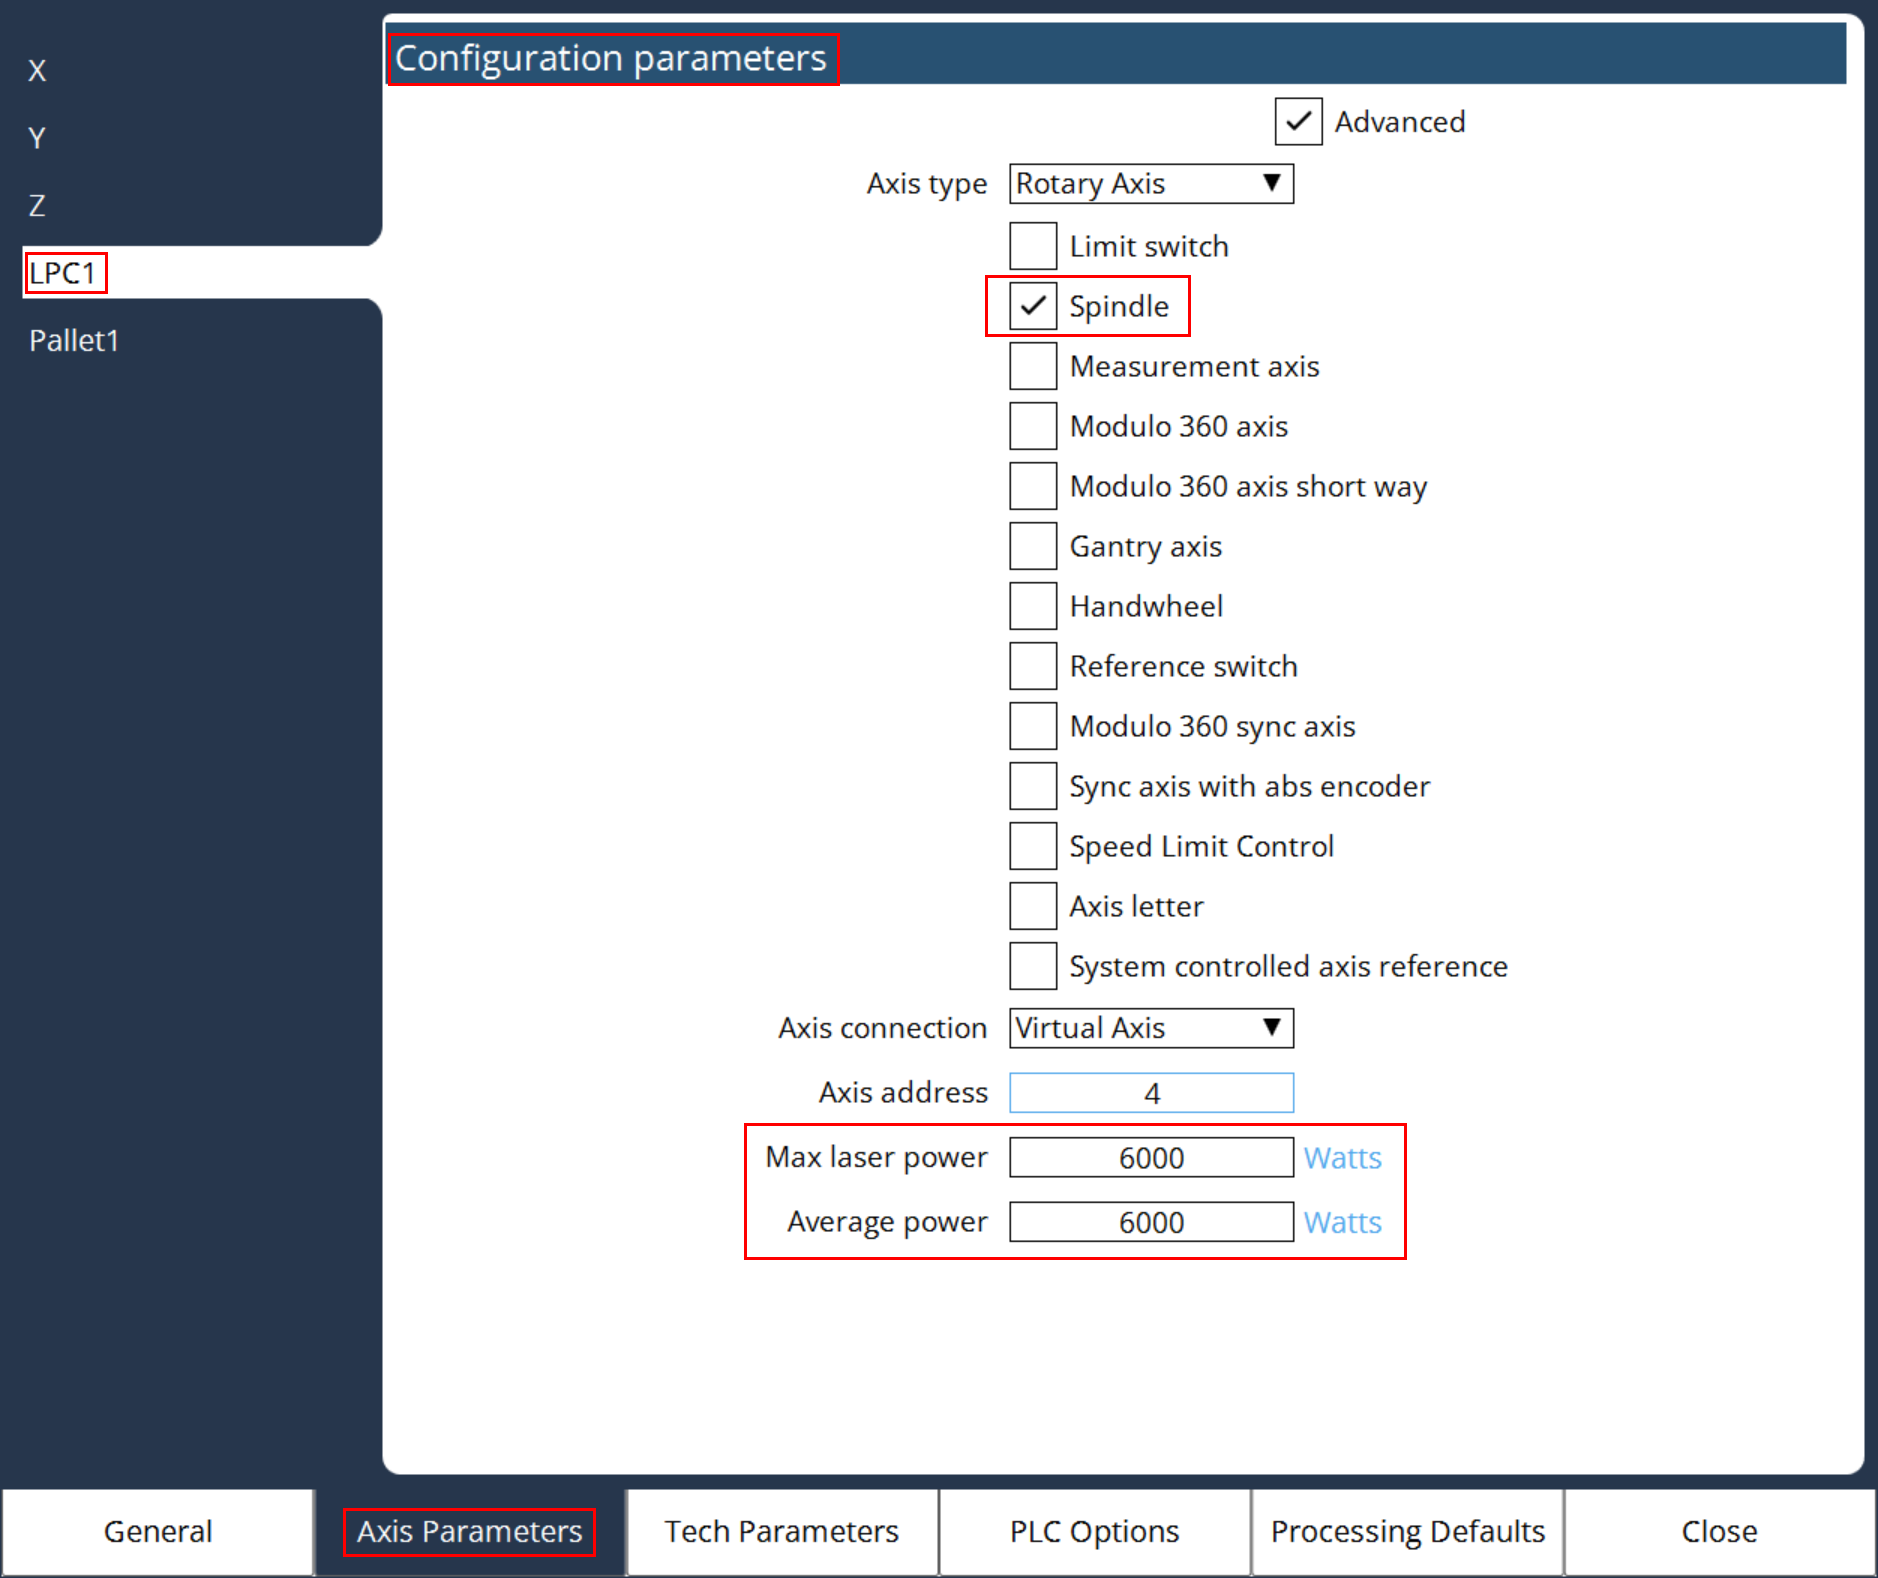
LPC Index Assignment
When LPC1 is selected, internally the MK Spindle Index Assignment is allocated with axis application index number.
Max Laser Power
The Max Laser Power value in Watts, internally updates the MK Spindle Speed which complies with a nominal output value of 10V, via the axis analogue output. Hence, 4000 watts → 10V.
Average Power
The Average Power value in Watts, internally updates the MK Tech Spindle Speed Gear Stage1. It is only used for the information, to process the “High Peak Power” (HPP), type Laser source, where the scaling of analogue output will be varied depends on the process of Piercing/Cutting and it is handled internally in the PLC.
Max Laser Power = 5000 → 10v (HPP, used for Piercing)
Average Power = 3000 → 10v