Axes Correction File
In General parameters, Select Machine settings to access Axes correction file settings.
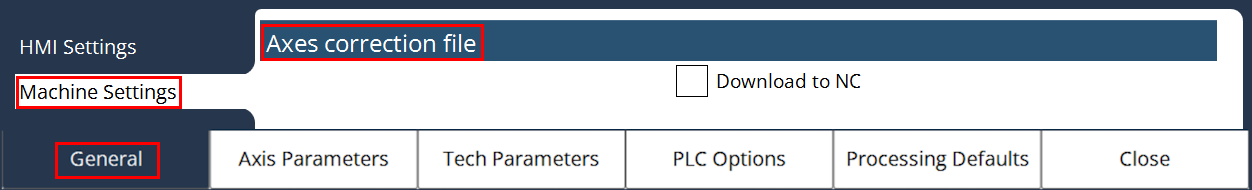
MK Axis Backlash Compensation sets the position correction (in mm or degrees) for axis direction reversal. Default is 0. Any non-zero value activates spindle reversal compensation.
Correction of a spindle inclination error: Errors are corrected using a table stored in flash PROM or sent from the PC after startup. Once loaded, correction is automatic for specified axes within a defined position range (relative to the reference point).
For recurring errors, modulo value defines a repeating correction range. At the end of this range, values loop back. Correction values range from -128 to +127 increments per position. Values are linearly interpolated between table points. No correction occurs outside the defined range. Max 4096 entries per axis.
Correction File Format: Stored as binary file AXIS.KOR in flash PROM.
Steps:
-
Enable "Download to NC".

-
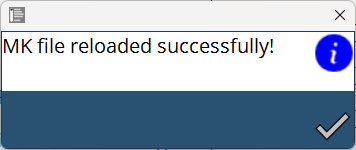
Click close to save and reload parameters.
-
If AXIS.KOR is present in the path C:\ProgramData\Metamation\Vulcan\Data. It will display as,
-
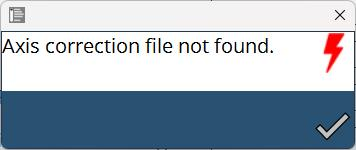
If AXIS.KOR is not present in the path C:\ProgramData\Metamation\Vulcan\Data. It will display as,
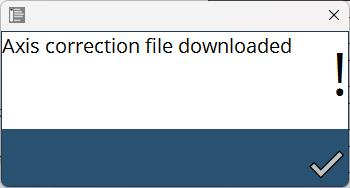
-
If "Download to NC" in axis correction file is disabled, above message will not be displayed.